How to Choose Hot Melt Adhesive Film for Nylon Fabric
Choosing a hot melt adhesive film for nylon fabric can become complicated when the bond fails, the laminate feels too stiff, or a coated fabric refuses to adhere. In our experience, selecting the right adhesive requires more than knowing that the substrate is nylon.
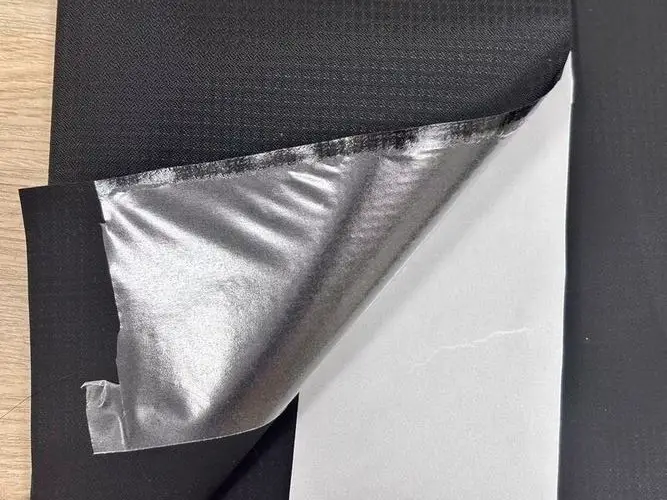
For nylon fabric, PA and selected TPU hot melt adhesive films are common starting options. PA is often worth evaluating for untreated, relatively stable nylon structures, while selected TPU grades are frequently considered for flexible or stretch laminates. The final choice should also account for coatings, the second substrate, process temperature and durability requirements, then be confirmed through actual lamination testing.
The better question is therefore not simply, “Which adhesive bonds nylon?” We need to understand the complete laminate before selecting the adhesive chemistry, grade, thickness and processing window.
What Is the Best Hot Melt Adhesive Film for Nylon Fabric?
There is no single hot melt adhesive film that is best for every nylon fabric.
PA and TPU are two common adhesive families worth evaluating, but they provide different starting points.
When Should You Consider PA Hot Melt Adhesive Film?
PA, or polyamide, hot melt adhesive film is often a strong starting candidate for untreated nylon fabrics because polyamide adhesives can have good chemical affinity with polyamide substrates.
This does not mean PA will always produce the strongest or most durable bond. Actual performance still depends on the adhesive grade, nylon construction, surface finish, second substrate and processing conditions.
PA may be worth evaluating when the nylon structure is relatively stable and the application prioritizes reliable textile bonding without requiring high elastic recovery.
For applications involving significant stretch, repeated flexing, washing or humid conditions, the final choice should be based on grade-specific durability testing rather than polymer family alone.
When Should You Consider TPU Hot Melt Adhesive Film?
Selected TPU hot melt adhesive grades are often considered when flexibility, softness or stretch compatibility is important.
TPU is a broad material family, so elasticity, hardness, recovery and durability can vary significantly between grades. Not every TPU adhesive film is highly elastic or equally suitable for textile lamination.
For nylon-spandex blends, stretch garments and other flexible structures, we usually evaluate whether the selected TPU grade can follow repeated fabric movement without creating a stiff bonding area.
For applications exposed to repeated washing, humidity or flexing, TPU chemistry and grade selection can also influence hydrolysis resistance and long-term durability. These properties should be verified under the intended end-use conditions.
For a broader look at TPU selection across different textile structures, see our TPU hot melt adhesive film guide for different fabrics.
PA vs. TPU Hot Melt Adhesive Film for Nylon Fabric
Both PA and TPU can be used in nylon textile bonding, but they provide different starting points for material selection.
| Selection Factor | PA Hot Melt Adhesive Film | TPU Hot Melt Adhesive Film |
| Untreated nylon | Often a strong starting candidate | Also suitable depending on grade |
| Flexible laminates | Grade-dependent | Selected flexible grades are often preferred |
| High-stretch applications | Requires careful grade selection | Selected elastic grades are often stronger candidates |
| Soft handfeel | Depends on grade and film thickness | Often easier to optimize with flexible grades |
| Repeated flexing | Must be evaluated | Selected grades may provide better fatigue compatibility |
| Coated or DWR nylon | Actual-material testing required | Actual-material testing required |
| Washing or humidity exposure | Grade-dependent | Selected grades may offer advantages depending on TPU chemistry |
| Second substrate | Critical | Critical |
| Final decision | Confirm by testing | Confirm by testing |
For untreated nylon, PA can be a logical first material to evaluate because of its affinity with polyamide substrates. For highly elastic nylon blends or applications where softness and repeated movement are important, selected TPU grades may provide a better mechanical match.
These are starting points rather than universal rules. The finished nylon, second substrate and production conditions should determine the final adhesive grade.
Why Is “Nylon Fabric” Alone Not Enough to Choose an Adhesive?
When a customer tells us only, “I need adhesive film for nylon,” we still do not have enough information to select a grade confidently.
Several variables can completely change the result.
Nylon Fabric Construction
A lightweight woven nylon behaves differently from a thick technical textile, knitted nylon or multilayer fabric.
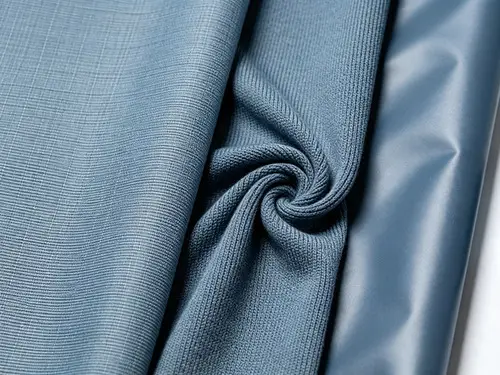
Fabric construction affects adhesive contact, penetration, heat transfer, flexibility and final handfeel.
A film thickness that works well on one nylon fabric may make another laminate unnecessarily stiff.
Stretch and Recovery
Some nylon fabrics have little stretch, while others contain spandex or are engineered for significant elongation and recovery.
When the laminate repeatedly stretches during use, the adhesive layer must tolerate that movement.
This is why we evaluate not only whether the adhesive stretches, but also whether the selected grade provides suitable recovery and durability under repeated deformation.
For stretch-focused projects, see our elastic hot melt adhesive film selection guide.
Coatings and Water-Repellent Treatments
This is one of the most important variables in nylon bonding.
Nylon fabric may contain:
- durable water-repellent treatment (DWR);
- waterproof coatings;
- resin finishes;
- printing layers;
- protective surface treatments;
- other functional finishes.
In these cases, the adhesive may actually contact the surface treatment rather than the underlying nylon fiber.
That can significantly change wetting and adhesion.
For treated nylon, we prefer testing the actual finished production fabric instead of selecting an adhesive only from the fiber composition.
Heat Sensitivity
Nylon may tolerate the selected process temperature while another component in the laminate does not.
Foam, elastic fibers, coatings, printed layers and polymer films can all introduce additional temperature limitations.
The processing window therefore needs to protect the complete laminate rather than only the nylon layer.
The Second Substrate
The second substrate is often one of the most important selection factors.
Instead of asking:
Which adhesive bonds nylon?
A more useful engineering question is:
Which adhesive bonds this nylon to this second material under the required production and end-use conditions?
That question gives us much more useful information for material selection.
How Does the Second Substrate Affect Adhesive Selection?
Nylon to Nylon
For nylon-to-nylon lamination, PA can be a logical starting candidate, particularly with untreated and relatively stable nylon structures.
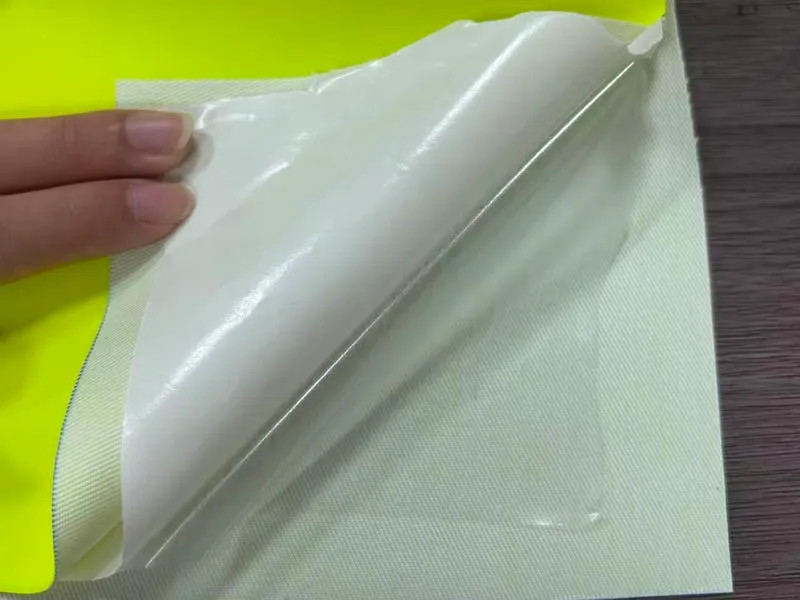
Selected TPU grades may also be evaluated when greater flexibility or softness is required.
Film thickness matters as well. Excessive adhesive can change the handfeel of lightweight nylon even when bond strength is acceptable.
Nylon to Spandex or Elastic Fabric
Elastic laminates place additional mechanical demands on the adhesive layer.
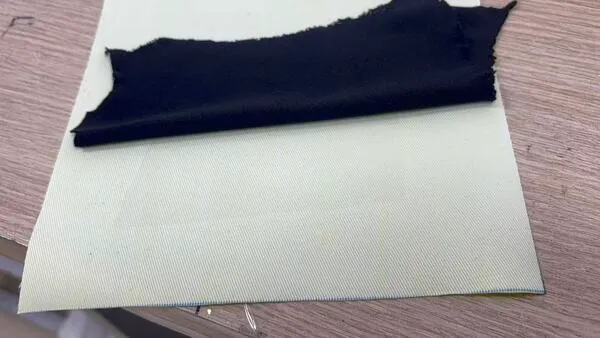
For nylon-spandex or other stretch structures, selected elastic TPU grades are often worth evaluating because the adhesive needs to follow repeated movement without becoming the rigid point in the laminate.
Initial bonding strength alone is not enough. Recovery and fatigue behavior should also be considered.
Nylon to Foam
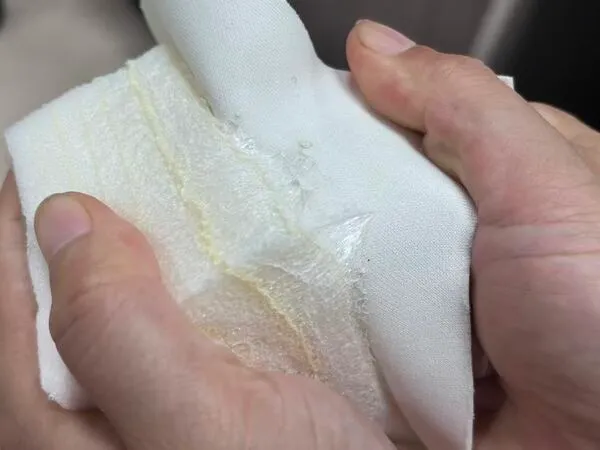
Foam introduces variables such as density, cell structure, surface condition and heat sensitivity.
An adhesive may bond nylon successfully while performing poorly on the foam side.
We therefore evaluate both surfaces and check whether the required lamination conditions cause the foam to shrink, soften or deform.
Nylon to TPU or Other Polymer Layers
Nylon may be laminated to TPU film, PVC, synthetic leather or other polymer layers.
In these structures, adhesive selection needs to account for both surfaces.
If either material has a coating or surface treatment, we also need to identify the actual bonding surface rather than assuming the adhesive directly contacts the base polymer.
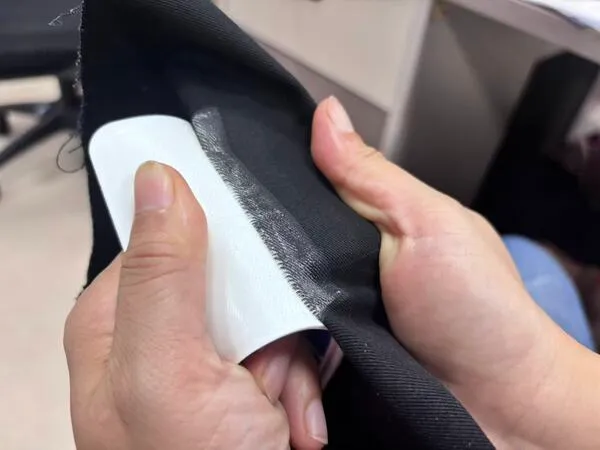
Nylon to Other Textiles
For nylon bonded to polyester, nonwoven materials or other textile structures, the adhesive needs to work across both surfaces while meeting the required flexibility and durability.
For a broader material-selection overview, see our hot melt adhesive film for textile fabric guide.
Does Water-Repellent or Coated Nylon Affect Bonding?
Yes. Coatings and surface treatments can significantly change nylon bonding behavior.
A water-repellent surface may reduce adhesive wetting, while some coatings can become the weak boundary layer in the final laminate.
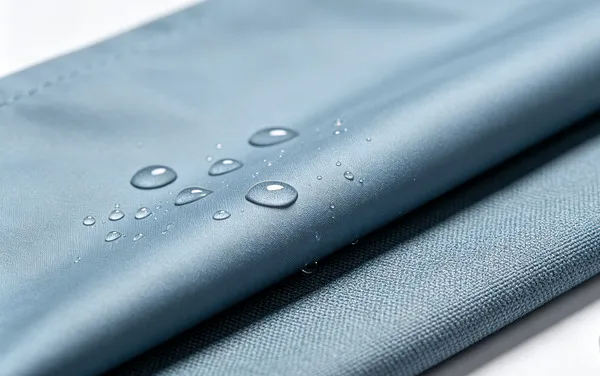
When coated nylon fails to bond properly, changing adhesive chemistry is only one possible solution.
We may also need to investigate:
- surface treatment chemistry;
- adhesive wetting;
- adhesive amount and thickness;
- lamination temperature;
- pressure and dwell time;
- coating-to-fabric adhesion.
This is why sending the actual finished nylon fabric is much more useful than sending only a material specification that says “100% nylon.”
What Temperature Is Required to Bond Nylon Fabric?
There is no universal lamination temperature for nylon fabric.
The correct processing window depends on the adhesive grade, adhesive melting behavior, nylon construction, surface treatment, second substrate, film thickness, pressure, dwell time and lamination equipment.
Higher temperature can sometimes improve bonding because it lowers adhesive viscosity and improves wetting of the textile surface. However, increasing temperature blindly can damage coatings, elastic fibers, foams, printed layers or other heat-sensitive components.
Heat must also transfer through the complete laminate before the adhesive reaches an effective bonding condition. A machine set temperature therefore does not necessarily represent the actual temperature at the adhesive interface.
We recommend treating supplier processing data as a starting window and confirming the final temperature, pressure and dwell time using the actual production materials.
Why Does Hot Melt Adhesive Film Fail on Nylon Fabric?
A failed bond does not automatically mean that the adhesive chemistry is wrong.
Poor Adhesive Wetting
If molten adhesive does not spread sufficiently across the bonding surface, the effective contact area may be too small.
Possible causes include insufficient heat, inadequate pressure, surface treatment or poor adhesive compatibility.
Surface Coating or Treatment
An adhesive that works on untreated nylon should not automatically be expected to perform the same way on DWR-treated or coated nylon.
The coating itself may become the actual bonding surface.
Insufficient Heat or Dwell Time
If the adhesive does not receive enough thermal energy, it may not melt and wet both substrates effectively.
Temperature, dwell time and heat transfer should therefore be evaluated together.
Excessive Heat
More heat is not always better.
Excessive temperature may damage coatings, foam, elastic fibers, printed layers or other heat-sensitive components.
Incorrect Film Thickness
Too little adhesive may provide insufficient coverage on rough or porous surfaces.
Too much adhesive may cause stiffness, squeeze-out or an undesirable handfeel.
Film thickness should therefore be matched to both substrate structure and final product requirements.
Mechanical Mismatch
A strong initial bond can still fail later if the adhesive and fabric behave differently under repeated movement.
This is particularly important for elastic nylon laminates.
The adhesive layer should be evaluated as part of the mechanical structure, not only as a bonding interface.
How Should Nylon Fabric Be Tested Before Production?
We prefer a material-validation process before moving into full production.
A practical sequence is:
- Identify both substrates and any surface treatments.
- Define stretch, softness, durability and processing requirements.
- Select candidate PA, TPU or other adhesive grades.
- Laminate the actual production materials under controlled conditions.
- Evaluate bonding using appropriate peel or tensile testing.
- Perform application-specific durability testing.
- Adjust adhesive grade, thickness or process conditions where necessary.
- Validate the final combination before mass production.
For elastic nylon laminates, initial peel strength alone may not be enough.
Repeated stretch or cyclic fatigue testing can help identify interface damage that only appears after the laminate has been flexed multiple times. This is particularly important for nylon-spandex fabrics, seamless garments, sportswear and other applications that experience repeated deformation during use.
Where relevant, we can compare the bond before and after cyclic stretching rather than relying only on the initial laminated sample.
Wash, heat or humidity testing should likewise reflect the actual end-use requirements instead of applying one universal test condition to every nylon laminate.
What Information Should You Send to an Adhesive Supplier?
The more complete the material information, the faster we can narrow down suitable adhesive options.
For nylon fabric projects, we normally want to know:
- nylon fabric construction;
- fiber composition and whether spandex is present;
- second substrate;
- coating, DWR or other surface treatment;
- required stretch and recovery;
- required softness;
- maximum acceptable process temperature;
- lamination equipment;
- washing or durability requirements;
- final application.
Whenever possible, samples of both production substrates are especially useful.
If TPU is being considered, you can also review our TPU hot melt adhesive film grades and specifications.
If you are searching for where to buy hot melt adhesive film for nylon fabric, we recommend evaluating suppliers based not only on available adhesive chemistry but also on their ability to review both substrates, provide samples and support lamination testing.
How Can VOMELT Help Select Adhesive Film for Nylon Fabric?
We prefer to start with the complete laminate rather than recommending one adhesive grade for every nylon application.
Our selection process can include:
- reviewing both substrates;
- checking surface treatments and heat limitations;
- understanding stretch and durability requirements;
- selecting candidate adhesive grades;
- preparing samples for evaluation;
- conducting lamination trials;
- evaluating bonding performance;
- adjusting material or process conditions where necessary.
Final temperature, pressure, dwell time, peel performance, wash resistance and durability should be confirmed using the customer’s actual materials and defined test conditions.
Frequently Asked Questions About Hot Melt Adhesive Film for Nylon
PA is often a strong starting candidate for untreated, relatively stable nylon, while selected TPU grades are frequently evaluated for flexible or stretch nylon laminates. Coatings, the second substrate, processing conditions and durability requirements can change the final choice, so actual-material testing is recommended.
Yes, PA hot melt adhesive film can be suitable for nylon and is often a logical starting candidate for untreated nylon substrates. However, adhesive grade, fabric construction, surface treatment, the second substrate and end-use conditions still determine actual bonding performance.
Yes. Selected TPU hot melt adhesive films can bond nylon fabrics and are often evaluated when flexibility, softness or stretch compatibility is important. TPU properties vary considerably by grade, so the selected material should be tested with the actual nylon and second substrate.
Some hot melt adhesives can bond nylon, but a conventional hot glue stick should not automatically be treated as equivalent to an industrial hot melt adhesive film. Industrial adhesive films provide controlled adhesive coverage and thickness, while the appropriate chemistry still depends on the substrates and application.
It may be possible, but coatings and water-repellent treatments can significantly alter adhesive wetting and bonding. The finished treated nylon should be tested because the adhesive may be contacting the surface treatment rather than the nylon fiber itself.
There is no single temperature suitable for all nylon laminates. The correct processing window depends on the adhesive grade, nylon structure, second substrate, film thickness, equipment, pressure and dwell time. Final conditions should be established using actual production materials.
For nylon-to-elastic-fabric lamination, selected flexible TPU grades are often worth evaluating. Adhesive elasticity should be matched to the laminate’s stretch and recovery, and repeated stretch or cyclic fatigue testing can provide more useful information than initial peel strength alone.
Final Takeaway
Choosing hot melt adhesive film for nylon requires more than matching an adhesive to the word “nylon.” Start with PA or selected TPU grades according to the laminate structure, then evaluate coatings, stretch, the second substrate, process limits and durability before confirming the final material through testing.